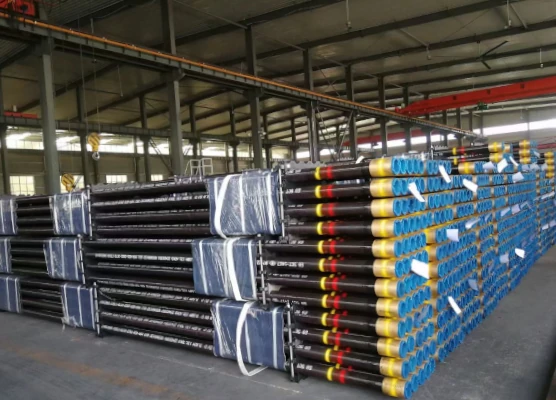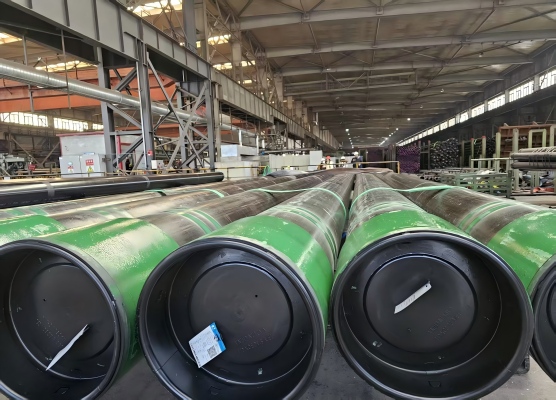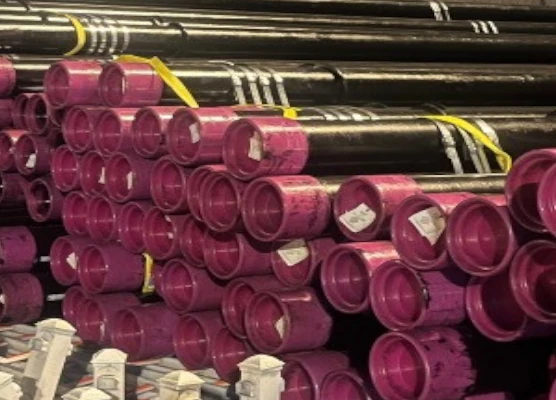


Oil tubing and casing (OCTG) work under extreme downhole conditions: high pressure, high temperature, tension, compression and corrosive media. Every batch must pass a full set of inspections in accordance with API Spec 5CT before delivery, to avoid well leakage, pipe rupture and costly well control risks. Below are all standard tests we perform.
1. Chemical Composition Analysis
Chemical analysis is carried out on ladle samples and product samples. We test carbon, manganese, phosphorus, sulfur, silicon and other alloy elements, to verify the steel grade matches the order requirement (K55, N80, L80, P110 etc.). For sour service grades, strict control of impurity elements is mandatory for H₂S cracking resistance.
2. Mechanical Property Tests
- Tensile Test: Yield strength, ultimate tensile strength, elongation
- Hardness Test: HRC / HB hardness, critical for L80 and sour service pipes
- Charpy Impact Test: Impact energy at specified temperature, to resist brittle fracture All mechanical samples are taken from finished pipes, heat-treated together with the pipe body.
3. Hydrostatic Pressure Test (Hydrotest)
100% hydrostatic testing for each pipe. The pipe is filled with water and pressurized to the API-specified test pressure, held for the required duration. No leakage, sweating or pressure drop is allowed. This proves the pipe body can withstand internal pressure in service.
4. Drift Test
A calibrated drift mandrel passes through the full length of the pipe. This test confirms the minimum inner diameter meets specification, ensuring downhole tools, pumps and wireline can run smoothly without sticking.
5. Non-Destructive Testing (NDT)
Full-body NDT inspection for surface and subsurface defects, no damage to the pipe:
- UT (Ultrasonic Testing): Detect internal laminations, wall-thickness defects
- MT (Magnetic Particle Testing): Check surface cracks, mainly for pipe ends and couplings
- ET (Eddy Current Testing): Fast screening for surface defects
- PT (Liquid Penetrant Testing): Supplementary inspection for thread surfaces
6. Thread & Coupling Inspection
This is one of the most critical tests for tubing (NUE / EUE / Premium threads):
- Thread gauging with API working gauges (ring gauge & plug gauge)
- Thread taper, lead, height, root radius visual & dimensional check
- Visual inspection for chipping, galling, scratches
- Make-up test for premium connections if required
7. Dimensional & Visual Inspection
- Outer diameter, wall thickness, length, straightness
- End squareness, bevel angle
- Full visual check for dents, scratches, roll marks, rust
- Marking verification: steel grade, heat number, API monogram, size, weight, grade
8. Additional Optional Tests (On Customer Request)
- SSC / HIC test for sour service (NACE TM0177 / TM0284)
- Corrosion test
- Third-party witness inspection (SGS, BV, etc.)
- Pre-shipment tally and packing inspection
Final Documentation
After all tests pass, we issue the official MTC (Mill Test Certificate) with heat traceability, test records and all inspection data for your QA & procurement archive.