

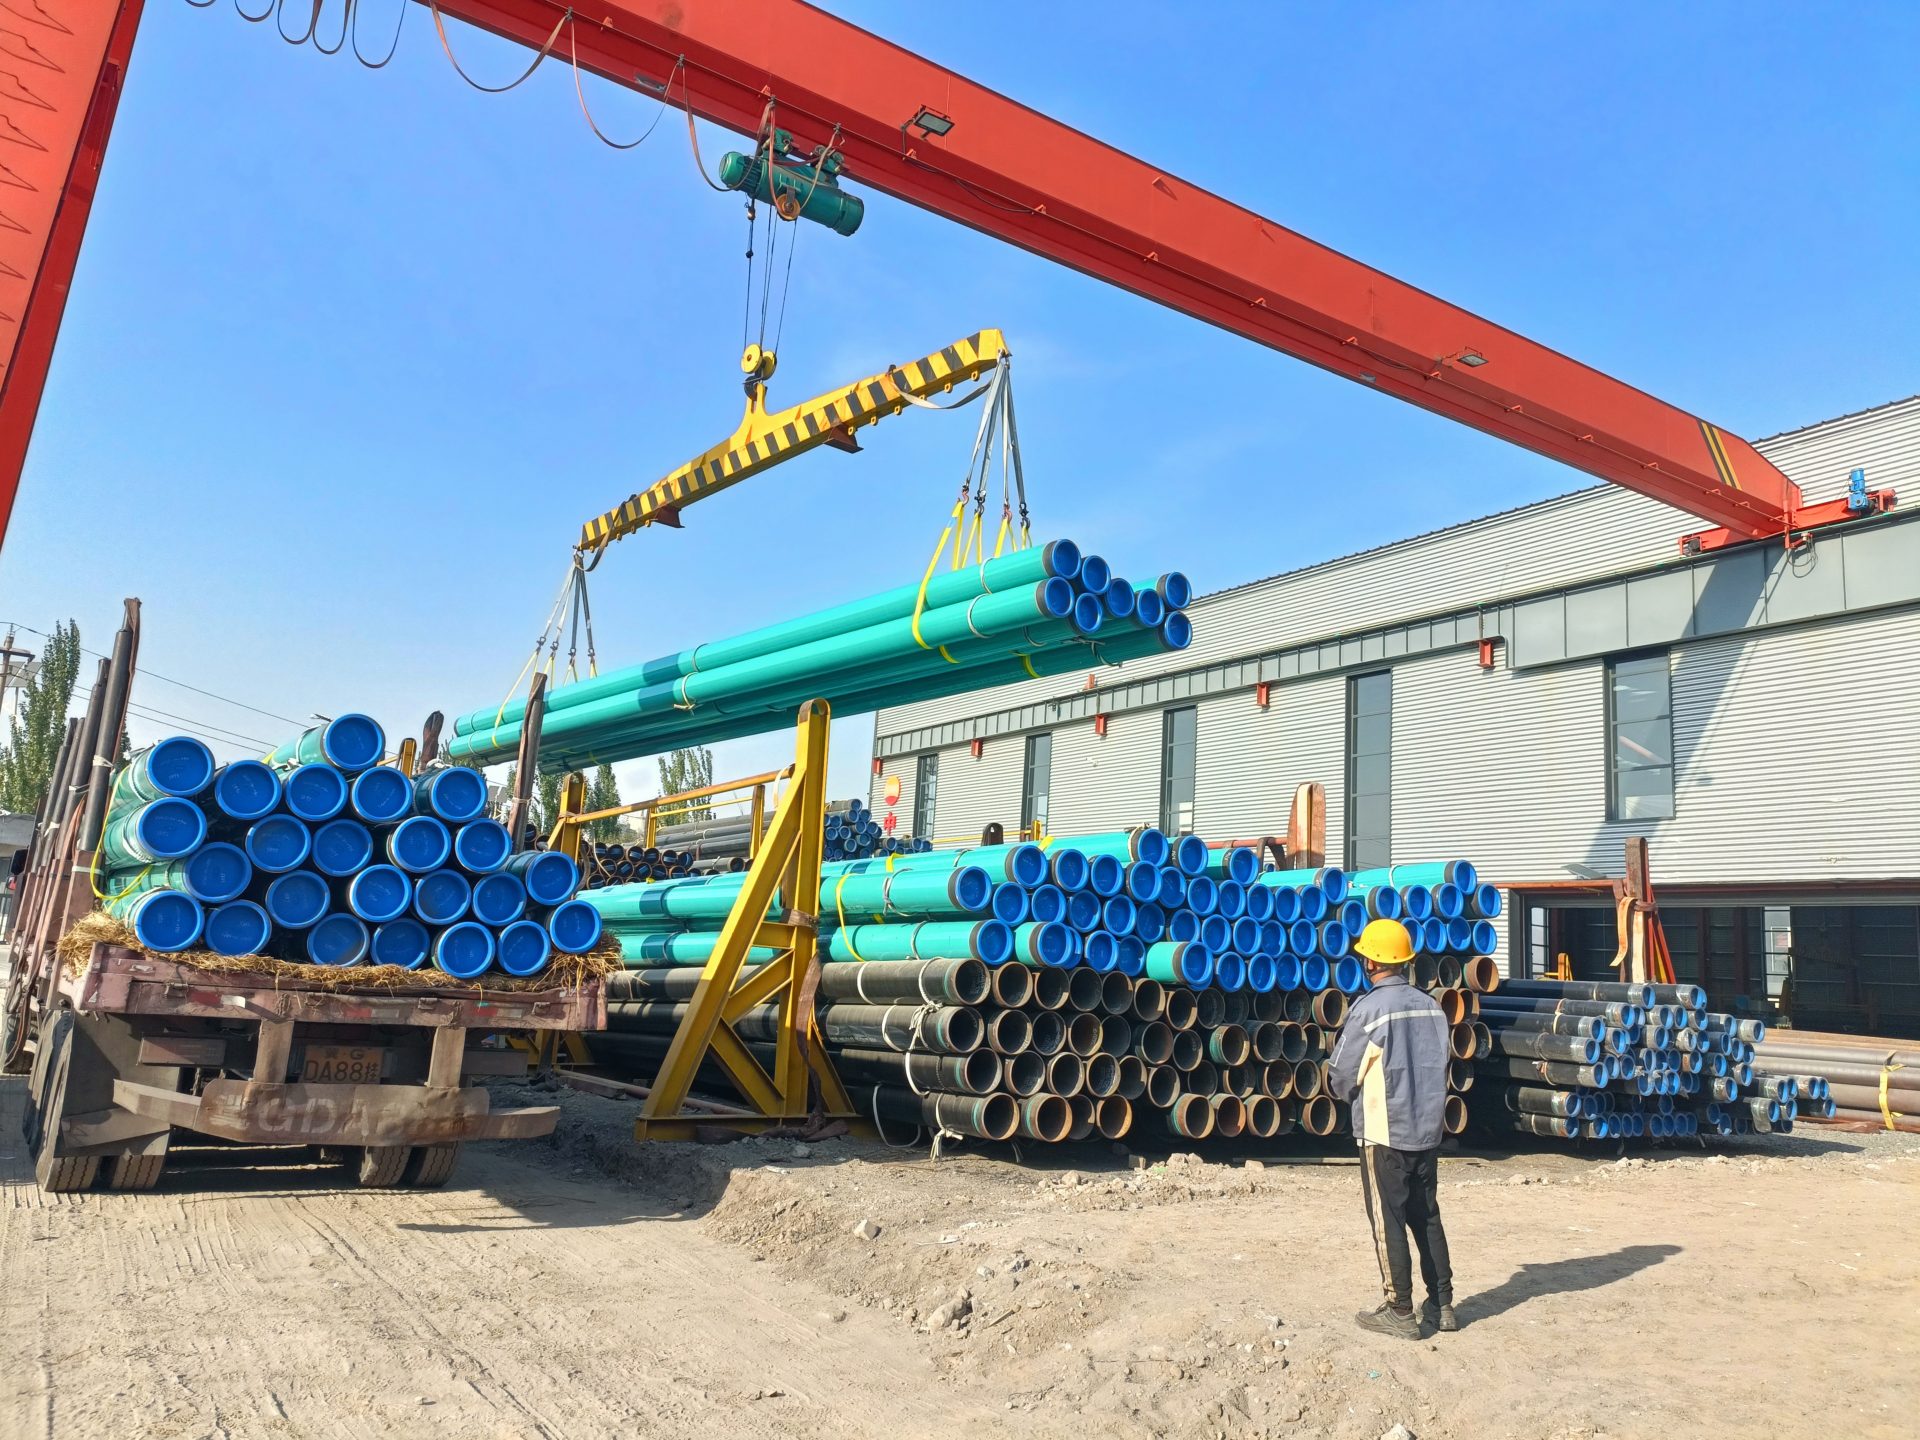
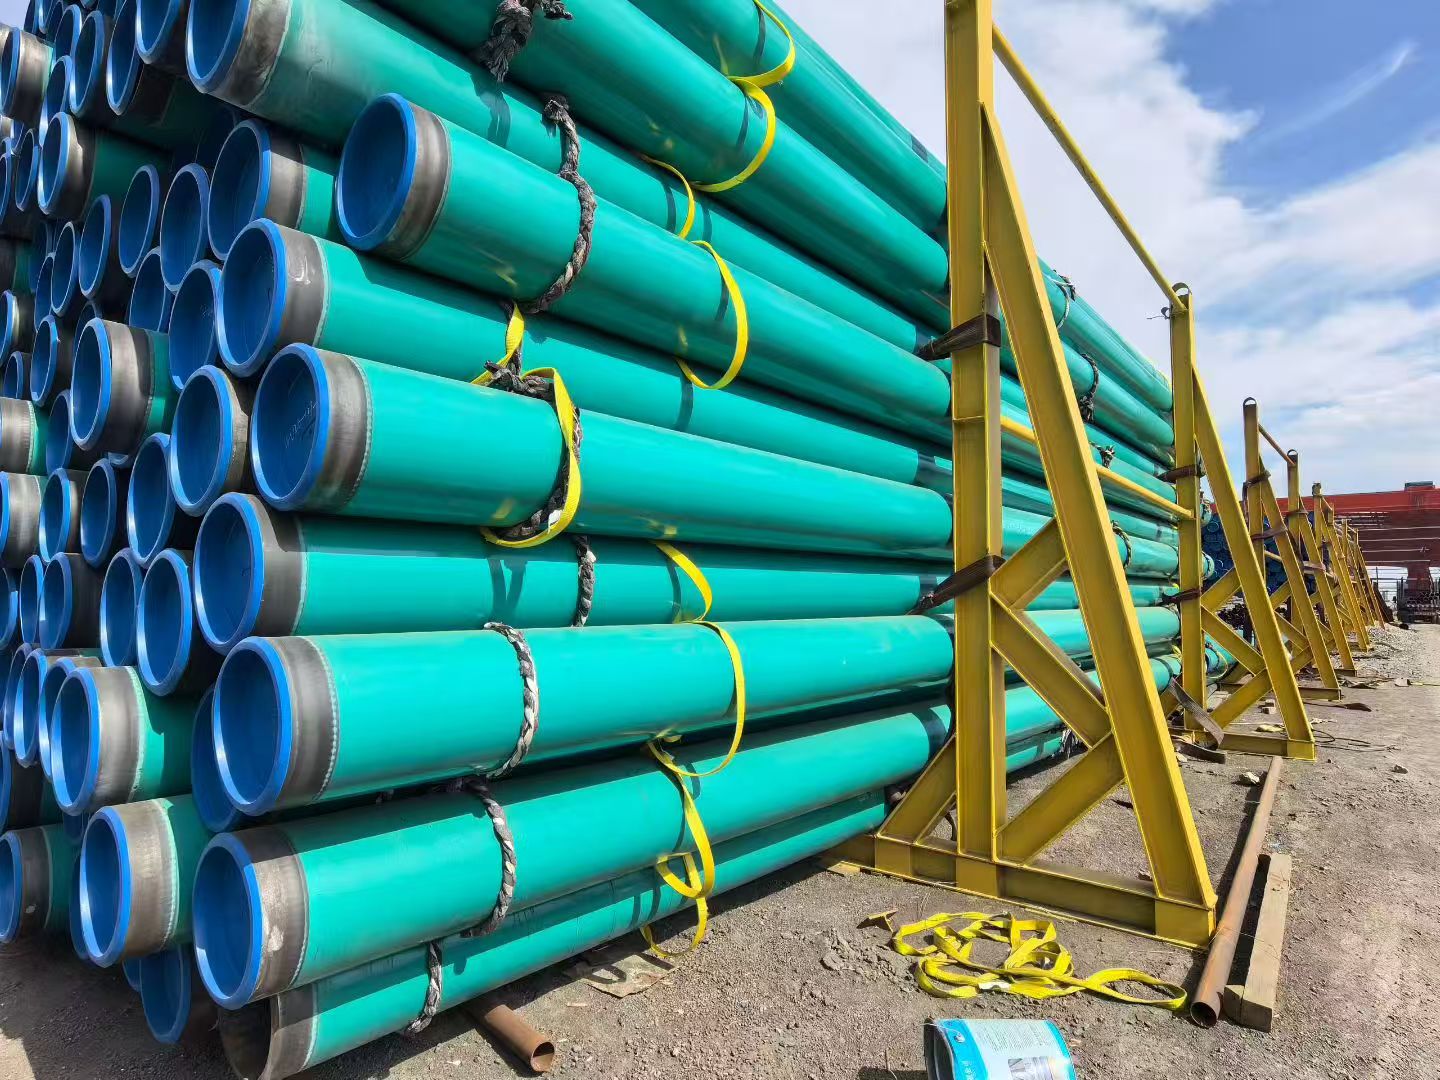
IMRI has successfully completed the delivery of 300 km of FBE (Fusion Bonded Epoxy) coated steel pipes for a major oil pipeline project in South America. The entire scope — from manufacturing, anti-corrosion coating application, quality inspection, customs clearance to export logistics — was executed within a tight 60-day window, meeting all client specifications and delivery milestones.


Project Challenge
The South American oil pipeline project posed several demanding requirements: 1.Tight delivery timeline: The client needed the full 300 km pipeline batch produced and exported within 60 days to keep their construction schedule on track. 2.Harsh field conditions: The pipeline route crosses corrosive soil and varying climatic zones, requiring long-term anti-corrosion performance that could guarantee decades of service life. 3.Stringent quality standards: FBE coating must meet international pipeline coating specifications, with uniform thickness, strong adhesion, and resistance to cathodic disbondment. 4.Complex export logistics: Coordinating production, third-party inspection, documentation, and ocean freight across borders without delay added execution complexity.
Our Solution
IMRI's engineering and export team mobilized immediately upon order confirmation: 1.Integrated production scheduling: Steel pipe manufacturing and FBE coating lines were prioritized and synchronized, eliminating idle time between stages. 2.High-performance FBE coating system: We applied a fusion bonded epoxy coating engineered for long-term corrosion protection, with excellent impact resistance, abrasion resistance, and cathodic shielding — built to withstand harsh downhole and field environments for sustained oil transmission. 3.In-process quality control: Coating thickness, adhesion, holiday detection, and dimensional inspection were conducted at each production stage, with third-party witness inspection arranged to client's specification. 4.Streamlined export execution: Our logistics team handled booking, documentation, customs declaration, and container loading in parallel with production, ensuring no gap between factory completion and vessel departure. The full 300 km FBE coated pipe shipment was delivered on schedule within 60 days, meeting all quality and compliance requirements. The client's trust reaffirms IMRI's robust manufacturing and export execution capability for global energy infrastructure projects. IMRI remains committed to supplying premium anti-corrosion pipeline products — FBE, 3PE, and API-spec steel pipes — to oil, gas, and water transmission projects worldwide.
Related products


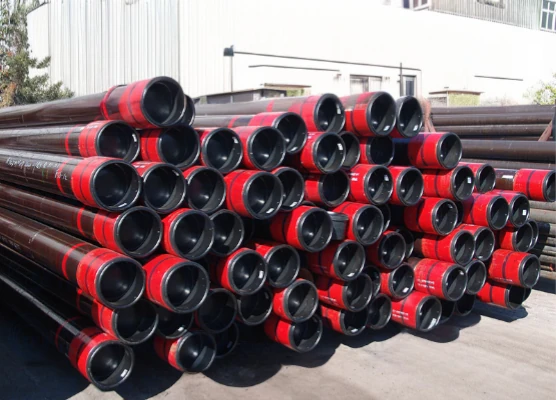
API 5CT L80-1 Casing for Deep Wells
Read More 
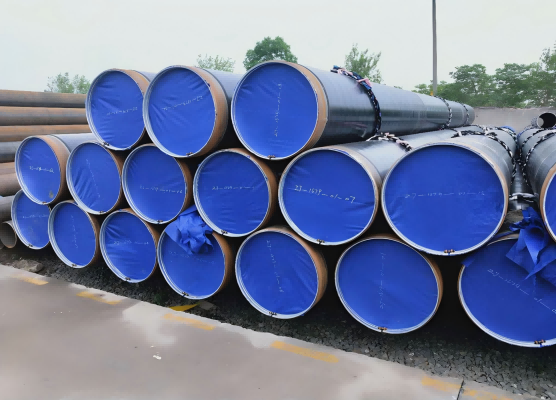
3PE Anti-corrosion Steel Pipe Epoxy Coating Reinforce Grade Gas
Read More
Premium 136RE HH Grade Railway Rail
Read More
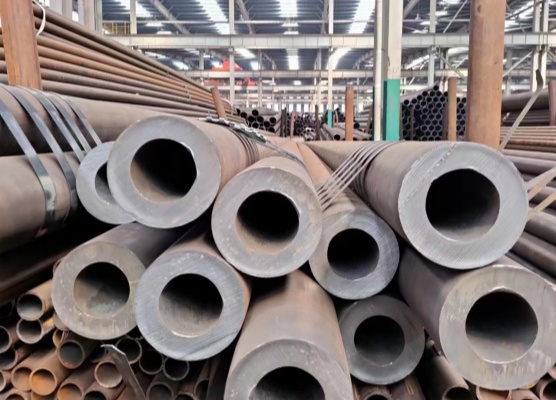
Grade P92 ASTM A335 Alloy Steel Pipe
Read More
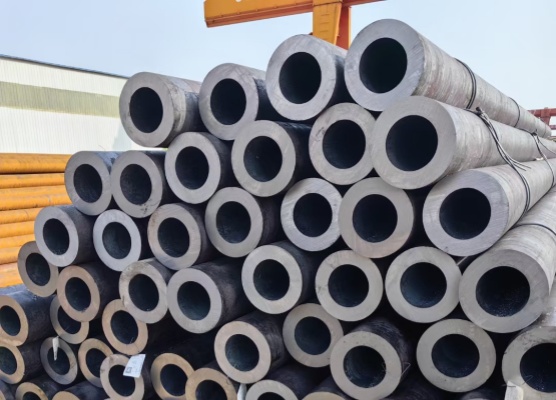
GB/T 3077-2015 Seamless Alloy Steel Pipe Grade 40Cr
Read More
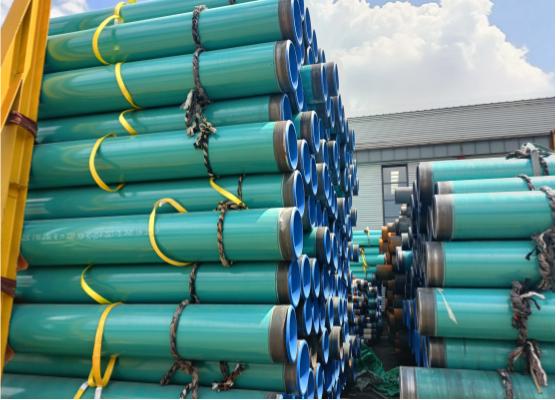
Heavy-Duty FBE Fusion Bonded Epoxy Coated Pipe
Read More
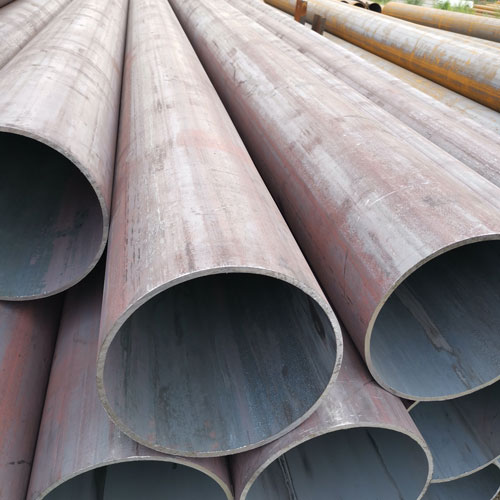
APL 5L X65 Oil and Gas Pipeline
Read More
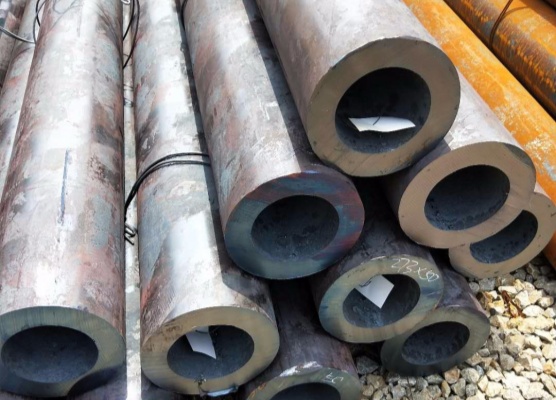
Grade P12 ASTM A335 Chromium-Molybdenum Alloy Pipe
Read More